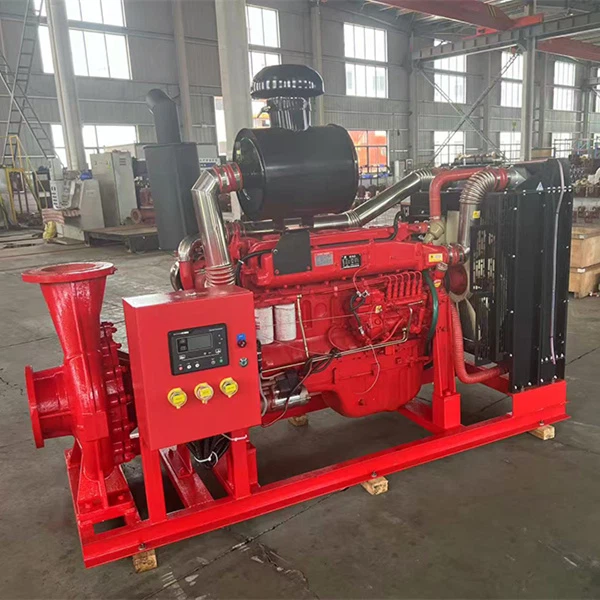
Engineered for Reliability and High Performance in Fire Protection
Meet the XBD series, our advanced single stage fire pump developed to address the specific demands of modern building fire protection systems. This product is rigorously designed to comply with the national standard GB6245-2006 and has been certified by authoritative testing centers, achieving leading domestic performance levels. It incorporates cutting-edge engineering to eliminate common failures like seizure after long idle periods, ensuring instant readiness. Characterized by high efficiency, low noise, minimal vibration, extended service life, and flexible installation options, this product offers a broad performance spectrum with smooth flow-head curves to prevent system overload.

Versatile Application for Fire and Combined Water Supply Systems

The primary mission of our single stage fire pump is to deliver water for fire suppression systems, including hydrant, sprinkler, and water mist systems. It is perfectly suited for a wide array of buildings such as residential complexes, hotels, office towers, commercial centers, and hospitals. Utilizing high-quality bearings, premium motors, and high-temperature resistant mechanical seals, it guarantees leak-free and secure operation. Beyond dedicated fire lines, its performance parameters are optimized to also handle domestic or production water supply, making it an ideal choice for combined fire-life/production water systems, as well as municipal and industrial water applications.
Choosing Between Horizontal and Vertical Configurations
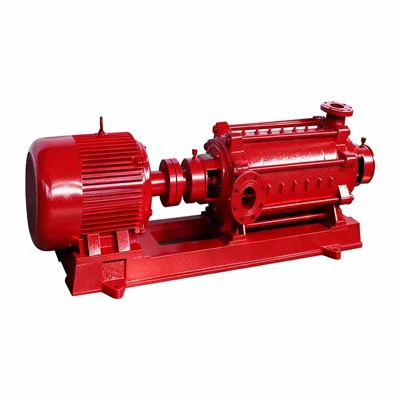
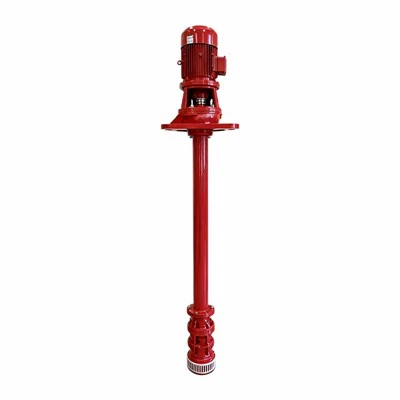
We offer both horizontal and vertical models to fit your spatial and performance needs. The robust horizontal single stage fire pump excels in scenarios demanding high flow rates and stable operation, such as large warehouses, factories, and stadiums. Its easy maintenance makes it perfect for ground-level pump houses. For space-constrained installations like high-rise buildings requiring higher pressure, our vertical model saves valuable floor space while ensuring dependable water supply to elevated floors. Our commitment to quality is evident in the use of ductile iron pump casings for strength, stainless steel impellers for efficiency and longevity, and our own factory-produced, full-copper, Class F155 insulated motors for unmatched reliability and thermal resilience.

|
Series |
Type |
Flow range |
Pressure range |
Matching power |
Caliber range |
Material |
Structural features |
Applicable Scenarios |
|
XBD-L Series |
Vertical single-stage fire pump |
1~100 L/S |
0.32~2.25 MPa |
1.5~200 KW |
φ32~φ350 mm |
Ductile iron, stainless steel |
Vertical compact: The pump shaft is vertical, which results in a small footprint, a large height, and a concentrated center of gravity. |
For space-constrained building projects, such as basements of high-rise buildings or small equipment rooms, vertical space can be fully utilized. |
|
Operating conditions: It exhibits strong stability under low flow and high head conditions; however, it experiences slightly greater vibration under high flow conditions. |
High-lift fire protection requirements: such as fire hydrants and sprinkler systems in high-rise buildings, meeting the requirements of low flow and high pressure. |
|||||||
|
Maintenance features: The motor/pump body needs to be vertically hoisted, and sufficient overhead operating space needs to be reserved for maintenance. |
Temporary fire protection system upgrade project: Flexible installation, can be quickly connected to vertical pipelines, and does not require large-scale ground modification. |
|||||||
|
XBD-W Series |
Horizontal single-stage fire pump |
10~140 L/S |
0.32~1.7 MPa |
7.5~280 KW |
φ160~φ350 mm |
Ductile iron, stainless steel |
Horizontal extension type: The pump shaft is horizontal, with a large lateral dimension, resulting in a large footprint, but a small height dimension. |
High-flow, low-head fire protection needs: such as main fire pumps for large buildings and district water supply systems. |
|
Operating conditions: The pump body and motor are horizontally distributed, the center of gravity is dispersed, and the operation is stable with low vibration and noise under high flow and low head conditions. |
For scenarios requiring high operational stability, such as data centers and hospitals, which require a low-vibration, low-noise environment. |
|||||||
|
Maintenance features: The horizontal layout eliminates the need for high-altitude operations to disassemble the motor and pump body, and makes it easier to replace parts (such as impellers and mechanical seals). |
Easy-to-maintain items: Ample maintenance space facilitates routine maintenance and parts replacement. |
Hot Tags: single stage fire pump, China single stage fire pump manufacturers, factory, fire fighting pump, fire pump priming system, flame pump, fire fighting pump pressure, diesel fire water pump, fire fighting diesel pump