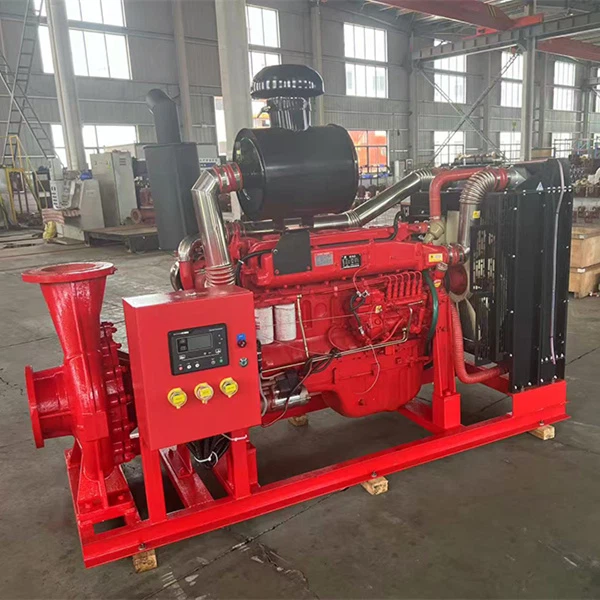
Introduction to Sewage Pumps
Sewage pumps are essential equipment in modern infrastructure, designed to transport wastewater, sewage, and other fluids containing solid particles from one place to another. They play a crucial role in municipal sewage systems, industrial wastewater treatment, and various other applications. These pumps need to be robust, reliable, and efficient to handle the challenging conditions associated with sewage, such as high solids content, corrosive substances, and varying flow rates.
Top 10 Sewage Pump Factories
1. Jiangsu Lixin Pump Industry Group Co., Ltd.
Jiangsu Lixin Pump Industry Group Co., Ltd. is a leading manufacturer of sewage pumps in China. With years of experience in the pump industry, the company has established a strong reputation for producing high - quality and reliable products.
The company's product range includes various types of sewage pumps, such as submersible sewage pumps, vertical sewage pumps, and self - priming sewage pumps. These pumps are designed to handle different sewage conditions, from domestic wastewater to industrial effluents.
Features in Sewage Pump Production
- Advanced Design: The company uses state - of - the - art design techniques to ensure that its sewage pumps have high efficiency and low energy consumption. For example, the impeller design is optimized to reduce clogging and improve the flow of sewage.
- High - Quality Materials: Jiangsu Lixin uses high - grade materials in the manufacturing of its pumps, such as stainless steel and cast iron, which are resistant to corrosion and wear. This ensures the long - term durability of the pumps, even in harsh sewage environments.
- Customization: The company offers customized solutions to meet the specific needs of different customers. Whether it is a small - scale domestic sewage system or a large - scale industrial wastewater treatment plant, Jiangsu Lixin can provide the appropriate pump model.
Advantages
- Technical Expertise: The company has a team of experienced engineers and technicians who are constantly working on improving the pump technology. They conduct in - depth research on fluid mechanics and pump design to develop more efficient and reliable products.
- Quality Control: Jiangsu Lixin has a strict quality control system in place. Every pump undergoes a series of tests before leaving the factory, including performance tests, leakage tests, and durability tests. This ensures that only high - quality products reach the market.
- After - sales Service: The company provides comprehensive after - sales service, including installation guidance, maintenance, and repair. Customers can rely on the company's support throughout the lifespan of the pumps.
Website: https://www.celixin.com/
2. Grundfos
Grundfos is a global leader in pump manufacturing, with a long - standing reputation for innovation and quality. The company was founded in 1945 in Denmark and has since expanded its operations worldwide.
Grundfos offers a wide range of sewage pumps, including submersible sewage pumps, dry - installed sewage pumps, and sewage treatment pumps. These pumps are used in various applications, such as municipal sewage systems, commercial buildings, and industrial facilities.
Features in Sewage Pump Production
- Energy - Efficient Technology: Grundfos is known for its energy - efficient pump designs. The company uses advanced motor technology and intelligent control systems to reduce energy consumption. For example, its pumps can adjust their speed according to the actual flow and pressure requirements, resulting in significant energy savings.
- Smart Monitoring and Control: Grundfos' sewage pumps are equipped with smart monitoring systems that can detect and diagnose problems in real - time. This allows for proactive maintenance and reduces the risk of pump failures.
- Robust Construction: The pumps are built with high - quality materials and a robust design to withstand the harsh conditions of sewage handling. They are resistant to corrosion, abrasion, and clogging.
Advantages
- Global Presence: Grundfos has a large network of sales and service centers around the world. This ensures that customers can easily access the company's products and services, no matter where they are located.
- Research and Development: The company invests heavily in research and development to continuously improve its pump technology. It collaborates with leading universities and research institutions to stay at the forefront of the industry.
- Sustainable Solutions: Grundfos is committed to sustainability. Its sewage pumps are designed to minimize environmental impact, such as reducing energy consumption and waste generation.
3. Xylem
Xylem is a well - known water technology company that offers a comprehensive range of sewage pump solutions. The company has a global footprint and serves customers in various industries, including municipal, industrial, and commercial sectors.
Xylem's sewage pumps are designed to handle a wide range of sewage applications, from small - scale residential systems to large - scale wastewater treatment plants. The company's product portfolio includes submersible sewage pumps, dry - pit sewage pumps, and grinder pumps.
Features in Sewage Pump Production
- Innovative Grinder Technology: Xylem's grinder pumps are equipped with advanced grinding mechanisms that can break down solid particles in sewage. This helps to prevent clogging and ensure smooth operation of the pump system.
- High - Performance Impellers: The impellers in Xylem's sewage pumps are designed for high efficiency and low NPSH (Net Positive Suction Head) requirements. This allows the pumps to operate effectively even in low - pressure conditions.
- Integrated Control Systems: Xylem offers integrated control systems for its sewage pumps, which can optimize the pump operation based on the flow and level of sewage. This improves the overall efficiency of the system.
Advantages
- Industry Experience: Xylem has decades of experience in the water technology industry. This experience allows the company to understand the specific needs of different customers and provide customized solutions.
- Product Range: The company offers a wide range of sewage pump products, which can meet the diverse requirements of various applications. Whether it is a simple domestic sewage pump or a complex industrial wastewater treatment pump, Xylem has a suitable solution.
- Technical Support: Xylem provides comprehensive technical support to its customers. Its team of experts can assist with pump selection, installation, and maintenance.
4. KSB
KSB is a German - based pump manufacturer with a long history of producing high - quality pumps. The company was founded in 1871 and has since become a global player in the pump industry.
KSB offers a variety of sewage pumps, including submersible sewage pumps, vertical sewage pumps, and horizontal sewage pumps. These pumps are used in municipal, industrial, and commercial applications.
Features in Sewage Pump Production
- Hydraulic Efficiency: KSB's sewage pumps are designed with high - efficiency hydraulic systems. The impellers and volutes are carefully engineered to ensure optimal flow and pressure characteristics, resulting in reduced energy consumption.
- Reliable Sealing Systems: The pumps are equipped with reliable sealing systems to prevent leakage. KSB uses advanced sealing materials and designs to ensure long - term sealing performance, even in harsh sewage environments.
- Modular Design: KSB's sewage pumps have a modular design, which allows for easy installation, maintenance, and upgrade. This reduces the downtime of the pump system and lowers the overall cost of ownership.
Advantages
- German Engineering: KSB is known for its German engineering expertise. The company adheres to strict quality standards and uses advanced manufacturing techniques to produce reliable and high - performance pumps.
- Global Service Network: KSB has a global service network that provides prompt and efficient after - sales service. Customers can rely on the company's service team for pump maintenance, repair, and spare parts supply.
- Product Innovation: KSB continuously invests in product innovation to meet the evolving needs of the market. It develops new pump technologies and features to improve the performance and efficiency of its sewage pumps.
5. Sulzer
Sulzer is a Swiss - based company that specializes in pump technology and services. The company has a strong presence in the sewage pump market and offers a wide range of products for different applications.
Sulzer's sewage pumps include submersible sewage pumps, dry - installed sewage pumps, and sewage treatment pumps. These pumps are designed to handle the challenges of sewage handling, such as high solids content and corrosive substances.
Features in Sewage Pump Production
- Advanced Materials and Coatings: Sulzer uses advanced materials and coatings in the manufacturing of its sewage pumps. For example, the pumps are coated with special anti - corrosion and anti - wear materials to extend their service life.
- Efficient Pumping Solutions: The company's sewage pumps are designed for high efficiency. They use advanced hydraulic designs and motor technologies to reduce energy consumption and improve the overall performance of the pump system.
- Custom - Built Solutions: Sulzer offers custom - built sewage pump solutions to meet the specific requirements of different customers. The company's engineering team can design and manufacture pumps based on the customer's application, flow rate, and pressure requirements.
Advantages
- Swiss Quality: Sulzer is known for its Swiss quality and precision. The company has a strict quality control system in place to ensure that its products meet the highest standards.
- Technical Expertise: Sulzer has a team of highly skilled engineers and technicians who have in - depth knowledge of pump technology. They can provide technical support and solutions to customers, from pump selection to system design.
- Global Reach: Sulzer has a global network of sales and service centers, which allows it to serve customers around the world. The company can provide timely and efficient service to its customers, no matter where they are located.
6. Flygt (a part of Xylem)
Flygt is a well - recognized brand in the sewage pump industry. It was acquired by Xylem in 2006 and has since become an important part of Xylem's product portfolio.
Flygt offers a wide range of sewage pumps, including submersible sewage pumps, mixer pumps, and aeration pumps. These pumps are used in various applications, such as municipal sewage treatment, industrial wastewater management, and stormwater drainage.
Features in Sewage Pump Production
- N - technology Impellers: Flygt's sewage pumps are equipped with N - technology impellers, which are designed to handle large solids and fibrous materials without clogging. The unique design of the impellers allows for efficient pumping of sewage with high solids content.
- Adaptive N - technology: The pumps use adaptive N - technology, which can adjust the impeller speed and performance based on the actual operating conditions. This ensures optimal pump operation and reduces energy consumption.
- Smart Pump Solutions: Flygt offers smart pump solutions that can be integrated with control systems. These solutions allow for remote monitoring and control of the pumps, improving the efficiency and reliability of the sewage system.
Advantages
- Brand Reputation: Flygt has a long - standing reputation for producing high - quality and reliable sewage pumps. The brand is well - known in the industry and is trusted by customers around the world.
- Innovation: Flygt is constantly innovating in the field of sewage pump technology. The company invests in research and development to develop new products and features that improve the performance and efficiency of its pumps.
- Comprehensive Product Range: Flygt offers a comprehensive range of sewage pump products, which can meet the diverse needs of different applications. Whether it is a small - scale residential sewage system or a large - scale industrial wastewater treatment plant, Flygt has a suitable pump solution.
7. Ebara
Ebara is a Japanese company that has been in the pump manufacturing business for over a century. The company offers a wide range of sewage pumps, including submersible sewage pumps, dry - installed sewage pumps, and sewage treatment pumps.
Ebara's sewage pumps are used in various applications, such as municipal sewage systems, industrial wastewater treatment, and building services.
Features in Sewage Pump Production
- High - Quality Manufacturing: Ebara uses high - quality materials and advanced manufacturing processes in the production of its sewage pumps. The pumps are built to last, with a focus on durability and reliability.
- Efficient Hydraulic Design: The company's sewage pumps have an efficient hydraulic design, which ensures high flow rates and low energy consumption. The impellers and volutes are optimized to provide smooth and efficient pumping of sewage.
- Low - Noise Operation: Ebara's sewage pumps are designed for low - noise operation. This is especially important in applications where noise pollution needs to be minimized, such as in residential areas.
Advantages
- Japanese Quality: Ebara is known for its Japanese quality and attention to detail. The company adheres to strict quality control standards and uses advanced manufacturing techniques to produce high - performance pumps.
- Global Presence: Ebara has a global presence, with sales and service centers in many countries around the world. This allows the company to serve customers globally and provide timely support.
- Research and Development: Ebara invests in research and development to continuously improve its pump technology. The company is constantly exploring new materials and designs to enhance the performance and efficiency of its sewage pumps.
8. Wilo
Wilo is a German company that specializes in pump technology. The company offers a range of sewage pumps, including submersible sewage pumps, sewage lift stations, and wastewater treatment pumps.
Wilo's sewage pumps are used in various applications, such as residential, commercial, and industrial sewage systems.
Features in Sewage Pump Production
- Energy - Saving Technology: Wilo's sewage pumps are equipped with energy - saving technology. The company uses intelligent control systems and variable - speed drives to optimize the pump operation and reduce energy consumption.
- Compact Design: The pumps have a compact design, which makes them suitable for installation in limited spaces. This is especially useful in applications where space is a constraint, such as in basements or small buildings.
- Easy Maintenance: Wilo's sewage pumps are designed for easy maintenance. The pumps have accessible components and are designed to be serviced quickly and efficiently, reducing downtime.
Advantages
- German Engineering Excellence: Wilo is known for its German engineering excellence. The company uses advanced manufacturing techniques and high - quality materials to produce reliable and high - performance pumps.
- Customer - Centric Approach: Wilo focuses on providing customer - centric solutions. The company works closely with its customers to understand their needs and provide customized pump solutions.
- Sustainable Solutions: Wilo is committed to sustainability. Its sewage pumps are designed to minimize environmental impact, such as reducing energy consumption and waste generation.
9. Tsurumi
Tsurumi is a Japanese company that has been manufacturing pumps for over 70 years. The company offers a wide range of sewage pumps, including submersible sewage pumps, dewatering pumps, and sludge pumps.
Tsurumi's sewage pumps are used in various applications, such as construction sites, municipal sewage systems, and industrial wastewater treatment.
Features in Sewage Pump Production
- Robust Construction: Tsurumi's sewage pumps are built with a robust construction. The pumps are made of high - quality materials, such as cast iron and stainless steel, which are resistant to corrosion and wear.
- Anti - Clogging Design: The pumps are designed with an anti - clogging feature. The impellers and volutes are designed to prevent clogging by large solids and fibrous materials, ensuring smooth operation of the pump.
- High - Performance Motors: Tsurumi uses high - performance motors in its sewage pumps. The motors are designed to provide high torque and efficiency, allowing the pumps to handle challenging sewage conditions.
Advantages
- Japanese Quality and Reliability: Tsurumi is known for its Japanese quality and reliability. The company has a strict quality control system in place to ensure that its products meet the highest standards.
- Global Distribution Network: Tsurumi has a global distribution network, which allows it to serve customers around the world. The company can provide timely and efficient service to its customers, no matter where they are located.
- Product Innovation: Tsurumi is constantly innovating in the field of pump technology. The company invests in research and development to develop new products and features that improve the performance and efficiency of its sewage pumps.
10. Seepex
Seepex is a German company that specializes in progressive cavity pumps, which are widely used in sewage applications. The company offers a range of sewage pumps that are designed to handle viscous and abrasive fluids, such as sewage sludge.
Seepex's sewage pumps are used in various applications, such as municipal sewage treatment plants, industrial wastewater treatment, and food processing industries.
Features in Sewage Pump Production
- Progressive Cavity Technology: Seepex's sewage pumps use progressive cavity technology, which provides a smooth and continuous flow of sewage. The pumps are capable of handling high - viscosity fluids and solids without clogging.
- Low - Shear Pumping: The pumps offer low - shear pumping, which is important for handling delicate materials in sewage, such as biological sludges. This helps to preserve the integrity of the materials and prevent damage.
- Customizable Solutions: Seepex offers customizable solutions to meet the specific needs of different customers. The company can design and manufacture pumps based on the customer's flow rate, pressure, and viscosity requirements.
Advantages
- German Engineering and Quality: Seepex is known for its German engineering and quality. The company uses high - quality materials and advanced manufacturing processes to produce reliable and high - performance pumps.
- Industry Expertise: Seepex has extensive industry expertise in handling viscous and abrasive fluids. The company's engineers have in - depth knowledge of progressive cavity pump technology and can provide technical support and solutions to customers.
- Global Service Network: Seepex has a global service network that provides prompt and efficient after - sales service. Customers can rely on the company's service team for pump maintenance, repair, and spare parts supply.
Conclusion
The top 10 sewage pump factories in the world in 2026 represent a diverse range of companies from different countries, each with its own unique strengths and features. These companies are at the forefront of sewage pump technology, constantly innovating and improving their products to meet the evolving needs of the market.
Jiangsu Lixin Pump Industry Group Co., Ltd. stands out with its advanced design, high - quality materials, and customization capabilities. Grundfos is known for its energy - efficient technology and smart monitoring systems. Xylem offers innovative grinder technology and a wide product range. KSB's hydraulic efficiency and modular design are its key advantages. Sulzer uses advanced materials and coatings and provides custom - built solutions. Flygt's N - technology impellers and smart pump solutions are highly regarded. Ebara offers high - quality manufacturing and low - noise operation. Wilo focuses on energy - saving technology and easy maintenance. Tsurumi's robust construction and anti - clogging design are notable. Seepex's progressive cavity technology and low - shear pumping are its unique features.
Overall, these companies play a crucial role in ensuring the efficient and reliable operation of sewage systems around the world. Their products and services contribute to the proper management of wastewater, which is essential for environmental protection and public health. As the demand for sewage pump solutions continues to grow, these companies are likely to continue to invest in research and development to further improve their products and stay competitive in the global market.